Kinshofer KM622 Grab Bucket Main Pivot Pins – Machined to Order
Kinshofer KM622 Grab Bucket Main Pivot Pins Machined to Order
Replacement main pivot pins for a Kinshofer KM622 grab bucket can be machined to order from high-tensile chrome alloy steel, complete with grease ways and welded-on pin flanges. Simply Welding machined a set of replacement main pivot pins for a Kinshofer KM622 grab bucket. We machined the 65mm main pivot pins with an M48 x 3mm thread for a Kinshofer KM622 grab bucket, with laser profiled flanges welded on in our workshop, then wrapped and delivered them ready to fit. We keep these Kinshofer KM622 pivot pins, and the full pin and bush kits they make up, in stock.
Job Description
The customer needed new main pivot pins for a Kinshofer KM622 grab bucket, each 65mm in diameter with an M48 x 3mm thread.
Material Used
A high-tensile alloy steel with high strength, toughness and fatigue resistance, ideal for high-stress applications like this.
Machining to Length
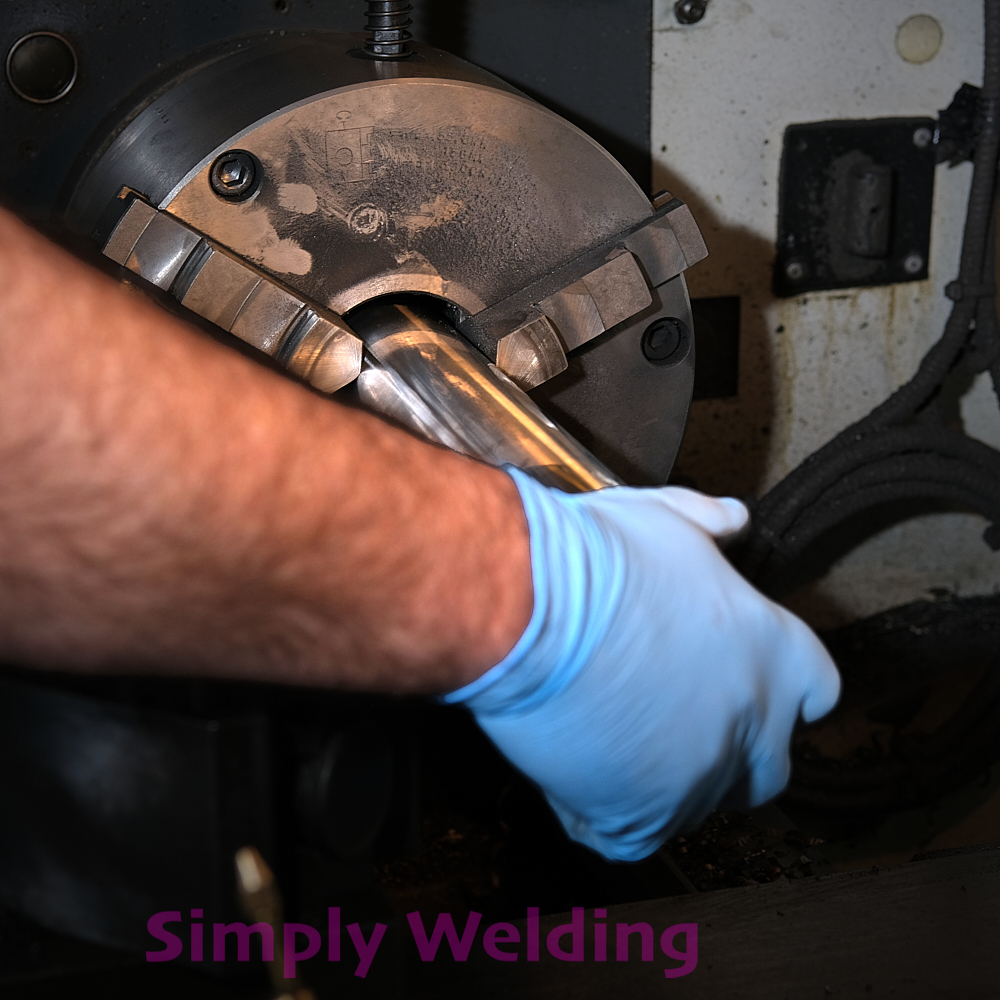
We faced off both ends and turned each pin to a finished length of 400mm.
Side One
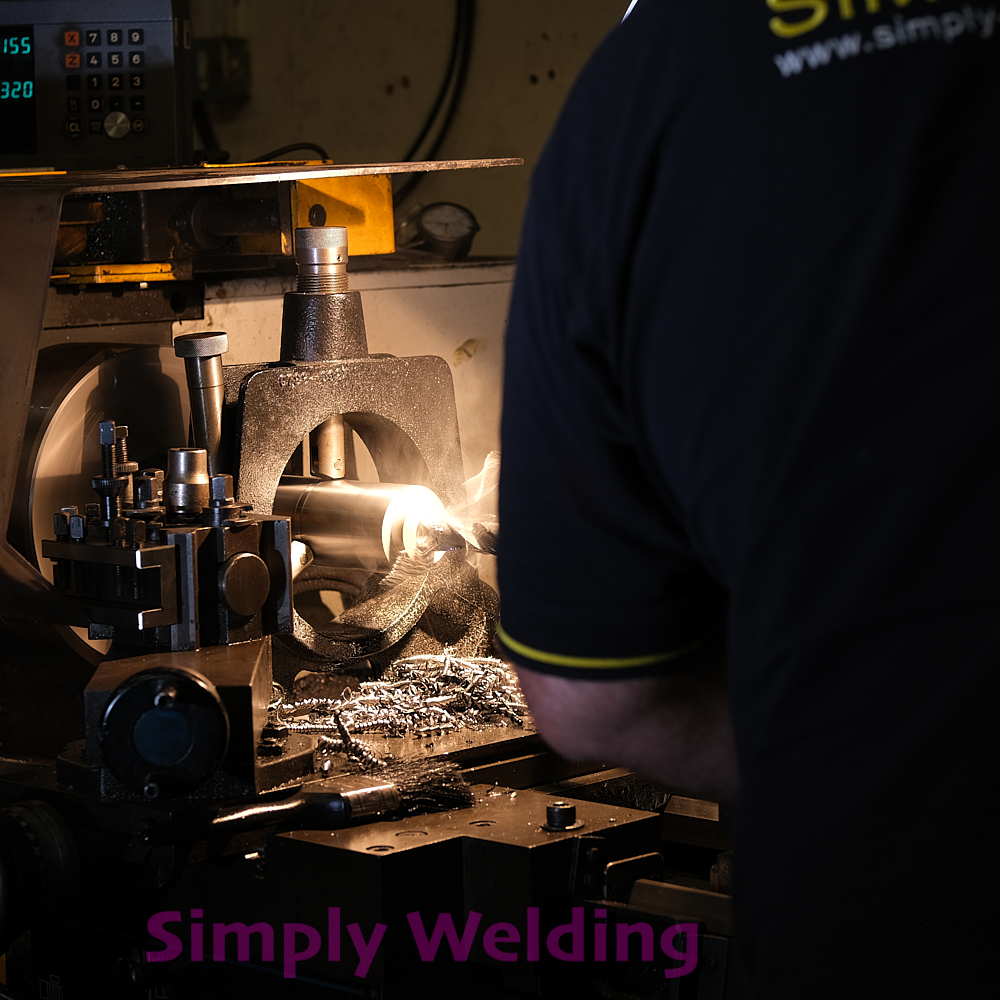
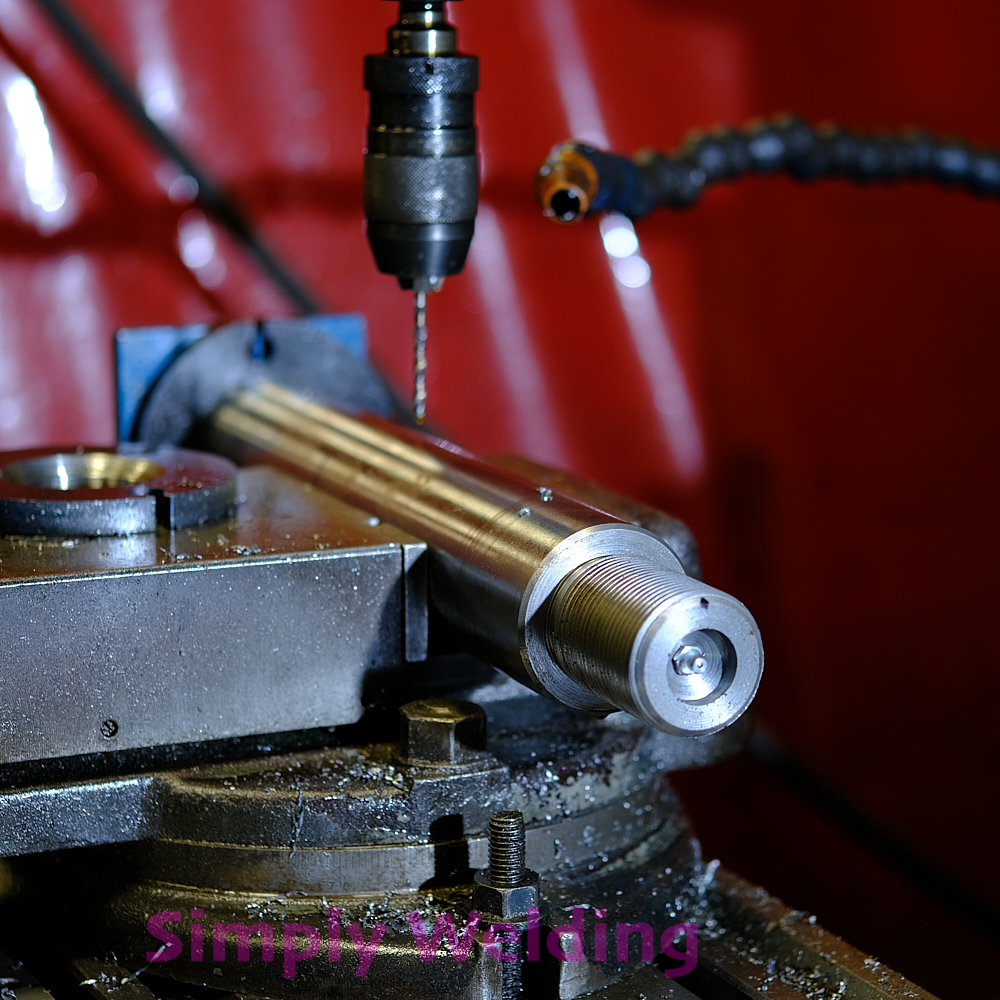
We machined the outside diameter of the threaded end to 48mm and chamfered the edges, then machined a thread relief and cut the 3mm pitch thread using the single-point method. A longitudinal grease hole was drilled 200mm deep, followed by a 24mm diameter x 20mm deep recess, which was threaded to take a 16mm grease nipple.
Side Two
We machined the outside diameter to 48mm and added a chamfer for weld preparation. This end also had a longitudinal grease hole drilled, plus a 24mm diameter x 20mm deep recess threaded for a 16mm grease nipple.
Grease Exit Holes
Four grease holes were drilled at set positions so grease could exit the pin and lubricate both the pin and the bronze bushes it runs in.
Pin Flanges
The pin heads (flanges) were laser profiled. We machined a weld preparation into each flange and bored the centre hole to give a friction fit on the pin, so the flange sat perfectly central before welding.
Welding the Pin Flanges
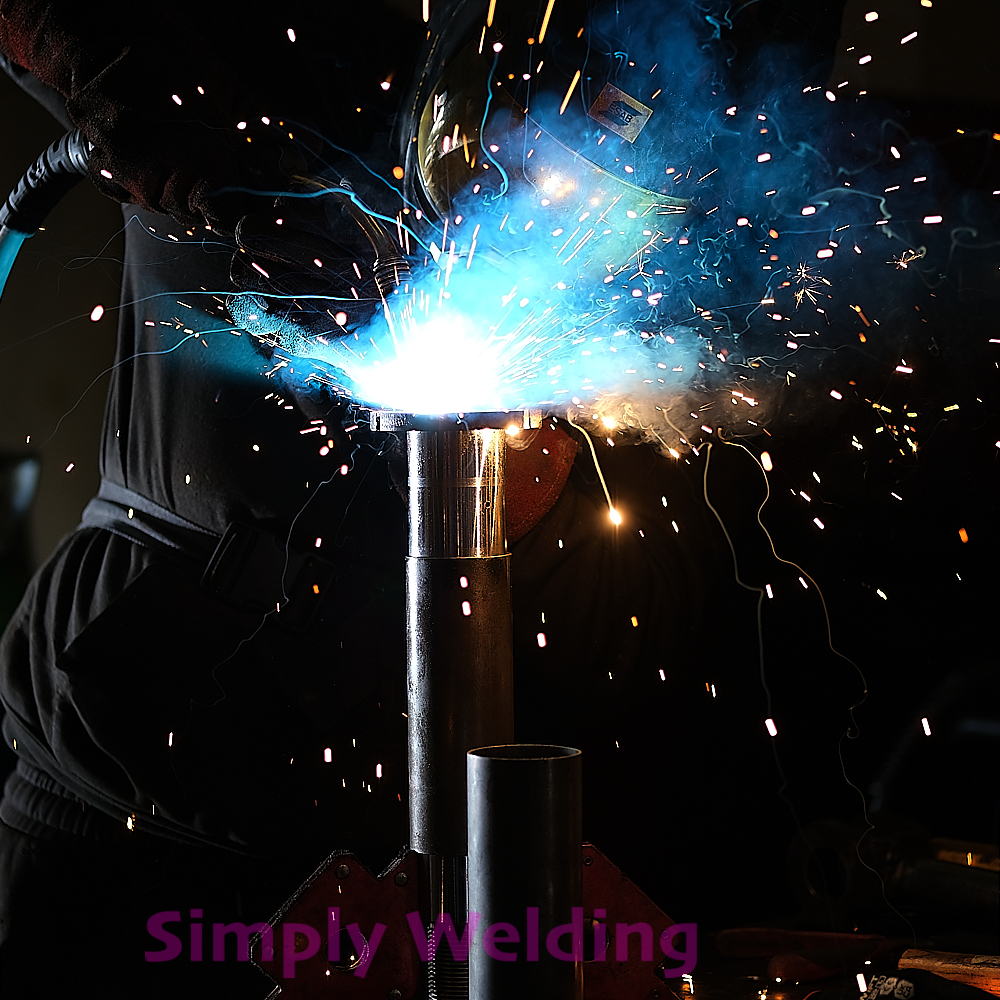
Each flange was warmed so it expanded enough to fit over the weld-prepared pin, then left to cool slightly so it gripped the pin. We then fully welded the flange to the pin using high-quality dual-shield welding wire.
Ready for Delivery
We painted the pin flanges, covered the exposed pins with cardboard tubes, partly wound on a 48mm full lock nut and wrapped each pin in protective film before delivering them to the customer.
Frequently Asked Questions
What size are Kinshofer KM622 main pivot pins?
The KM622 main pivot pins on this job were 65mm in diameter and 400mm long, with an M48 x 3mm thread on one end and a 48mm full lock nut. Each pin had a longitudinal grease hole and recesses threaded for grease nipples.
Can you machine replacement pivot pins to order?
Yes. We machine pivot pins to order in our workshop, turning, threading, drilling and tapping them to size, and welding on laser profiled flanges where the pin needs a head.
Do you stock Kinshofer KM622 pivot pins and pin and bush kits?
Yes. We keep Kinshofer KM622 main pivot pins in stock, along with the full pin and bush kits they make up, so worn pins and bushes can be replaced quickly.
Why do grab bucket pivot pins have grease holes?
A longitudinal grease hole runs through the pin, with exit holes drilled at set positions. This lets grease reach both the pin and the bronze bushes it runs in, reducing wear and extending the life of the pin and bushes.
How is the flange fitted to the pin?
The centre hole of the flange is bored to a friction fit. The flange is warmed so it expands over the weld-prepared pin, grips it as it cools so it sits perfectly central, and is then fully welded.
Want to see more of what we do?
Case Studies | Gallery
Need Kinshofer pivot pins or a pin and bush kit? Call 07747 682451 or send us some photos via WhatsApp.